
The snack packaging industry is changing as food manufacturers look for faster production, more accurate weighing, and packaging solutions that can handle different snack products.
From potato chips and nuts to candy, seeds, and mixed snacks, more manufacturers are investing in automatic snack sachet packing machines to reduce manual work and improve packaging consistency.
Among these solutions, multihead weigher granule packing machines are becoming an important choice for snack manufacturers. They combine automatic weighing and bag packaging, making them suitable for businesses that need consistent portion sizes and continuous production.
So, what are the latest developments in snack sachet packing machines, and what should manufacturers consider when choosing one?
1. More Precise Weighing to Reduce Product Waste
For snack manufacturers, inaccurate packaging weights directly impact production costs. While an "overweight" bag-containing more product than intended-might seem like a minor issue, in large-scale production, it can lead to significant product waste.
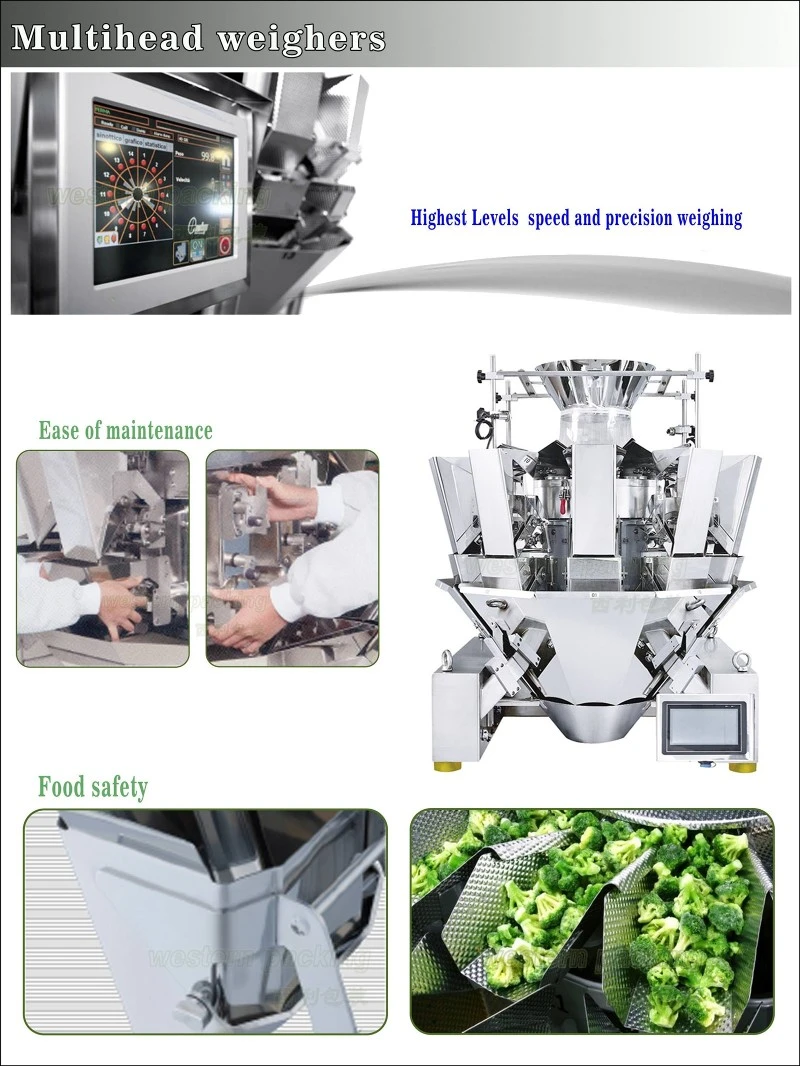
Multihead weighing technology facilitates more precise quantity control through automated, combinational weighing. This technology is particularly well-suited for products such as almonds, cashews, peanuts, sunflower seeds, and snack mixes-items where individual pieces often vary in size and weight.
Actual weighing accuracy depends on product characteristics, target weight, and equipment configuration.
2. Deep integration of feeding, weighing and packaging
Modern snack packaging is shifting from standalone machine operations toward integrated production lines.
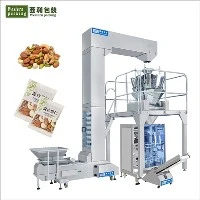
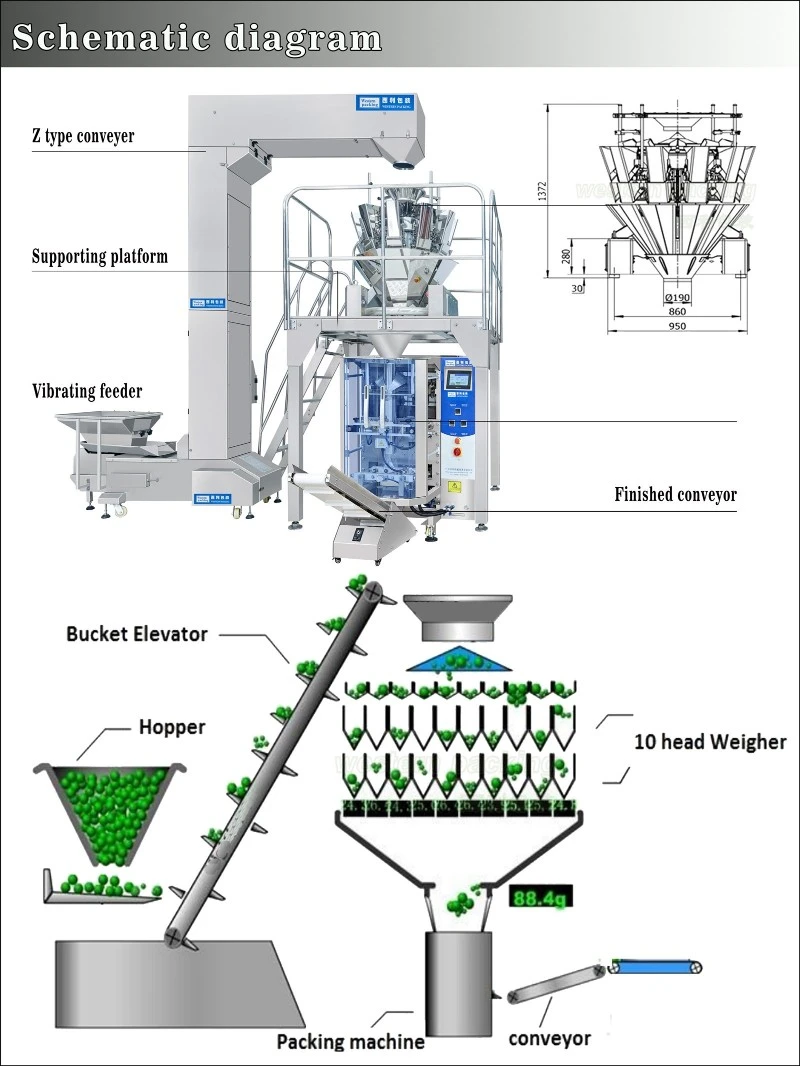
A typical system incorporates a Z-type bucket elevator, a storage hopper, a combination scale (multihead weigher), a vertical packaging machine, and a finished-product conveyor belt. The elevator transports the product to the weighing system, the combination scale performs precise, automated portioning, and the packaging machine handles bag forming, filling, sealing, and cutting.
The seamless coordination between these units not only ensures a stable supply of product but also minimizes the need for manual handling. For manufacturers planning to scale up their operations, an integrated packaging line also makes future capacity upgrades significantly easier to implement.
3. Improved Sealing and Packaging Protection
Packaging quality is just as important as weighing accuracy. Snack foods-such as potato chips, nuts, and puffed snacks-are highly sensitive to moisture and oxygen; therefore, a high-quality seal is essential for maintaining product integrity during storage and transport.
Modern snack packaging machines focus on achieving stable heat sealing, precise film positioning, and consistent bag formation. For products requiring enhanced preservation, packaging systems can also be equipped with a nitrogen-flushing feature to reduce oxygen levels inside the bag.
To ensure reliable packaging results, sealing temperatures and packaging films should be tested specifically for each product and material.
How to Choose the Right Snack Sachet Packing Machine?
Selecting the right equipment begins with a thorough understanding of your product and production requirements. Different types of snacks have distinct feeding characteristics; for instance, potato chips require careful handling to minimize breakage, while nuts and seeds demand a stable feeding process and precise weighing.
Before making a purchase, you should clearly define the product type, target fill weight, bag dimensions, packaging format, and desired production speed. Additionally, consider whether any supplementary features-such as nitrogen flushing for freshness or date printing-are required.
Providing these details to equipment manufacturers will help determine the optimal configuration for your multihead weigher, feeding system, and packaging machine.